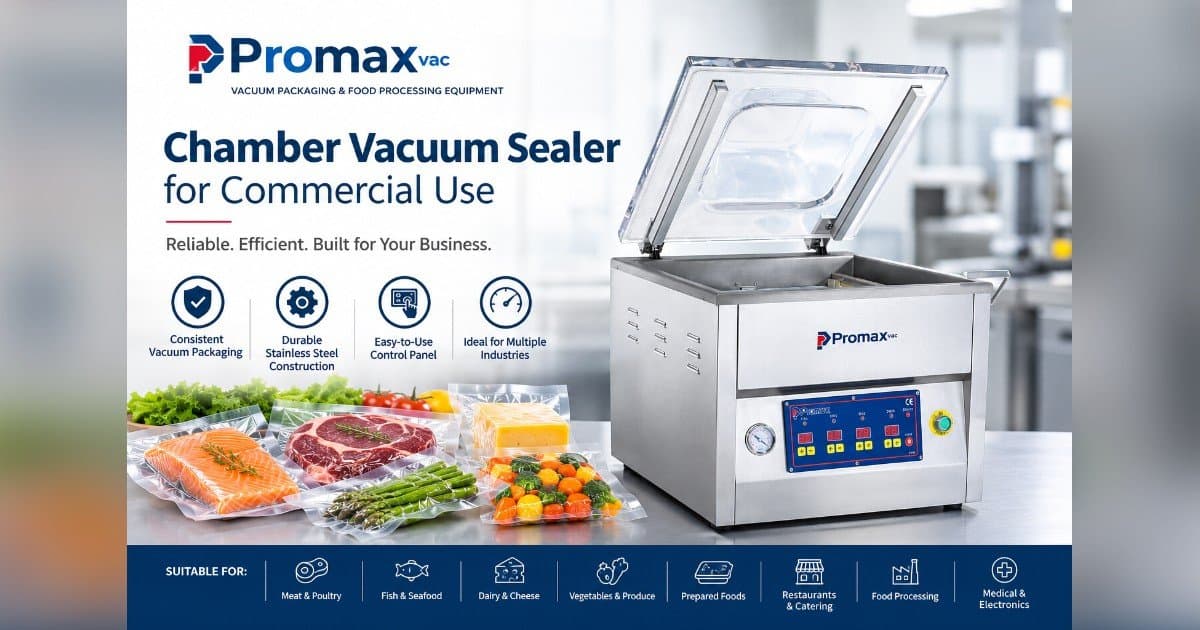
Commercial packaging operations weighing chamber vacuum sealers now have a clearer framework for equipment selection, as Ontario, California-based manufacturer Promarksvac Corp. outlines the factors that typically shape purchasing decisions in this category. The guidance arrives as food processors, distributors, and non-food manufacturers review their packaging lines and evaluate machines built for controlled air removal and consistent seals.
The distinction matters because chamber machines work differently from nozzle-style sealers. A chamber vacuum sealer places both the product and its pouch inside a sealed chamber, removing air from the entire chamber rather than drawing it out of the pouch through a nozzle. The pouch is heat sealed before the chamber returns to normal pressure. Because pressure inside and outside the pouch stays balanced during the cycle, the method is widely used for products containing liquids or moisture, including marinated proteins, brined products, and prepared meals. For operations packaging wet or liquid-heavy goods, that design difference can directly affect seal reliability and product presentation.
Configuration is another practical consideration. Tabletop models suit smaller kitchens, retail meat counters, and lower-volume production, while single-chamber floor models are used where larger products or higher daily volumes are involved. Double-chamber designs allow an operator to load one chamber while the other completes its cycle, a feature that can matter in continuous production settings. Belt-type and nozzle-type machines address other workflows within the broader vacuum packaging equipment category.
Packaging managers comparing commercial vacuum packaging machines generally weigh several practical points, according to the company: chamber dimensions and seal bar length relative to product and pouch size; pump capacity and cycle time relative to daily volume; compatibility with the pouch material and thickness in use; cleanability and hygiene requirements for the production environment; applicable electrical and sanitation certifications; and the availability of spare parts, manuals, and technical support. These factors can influence throughput, downtime, and long-term operating costs, making them relevant to both small processors and high-volume plants.
Promarksvac Corp. has manufactured vacuum packaging machines and food processing equipment since 1989. Its range of industrial vacuum packaging equipment includes tabletop, single-chamber, double-chamber, belt, and nozzle-type machines. Selected systems are equipped with Busch vacuum pumps and are available with applicable UL, ETL, and NSF certifications. The company also offers rollstock packaging machines, MAP tray sealers, commercial shrink tanks, heat sealers, vacuum seal bags, and spare parts, along with processing equipment such as vacuum tumblers, brine injectors, and piston stuffers.
The equipment is designed for applications involving meat, poultry, seafood, cheese, and ready-to-eat meals, as well as medical and healthcare packaging. Manufactured in the USA and shipped worldwide, the company is the parent of Foodmax, Profood, and the Promarks Heat Seal Division. Product information, machine manuals, and demonstration videos are available at https://promarksvac.com, and media inquiries can be directed through the company's Email Contact.
